What We Offer

OUR PRODUCTS

Professional research, development, production and sales of various low and medium pressure valves
About Us

LITTLE BOY

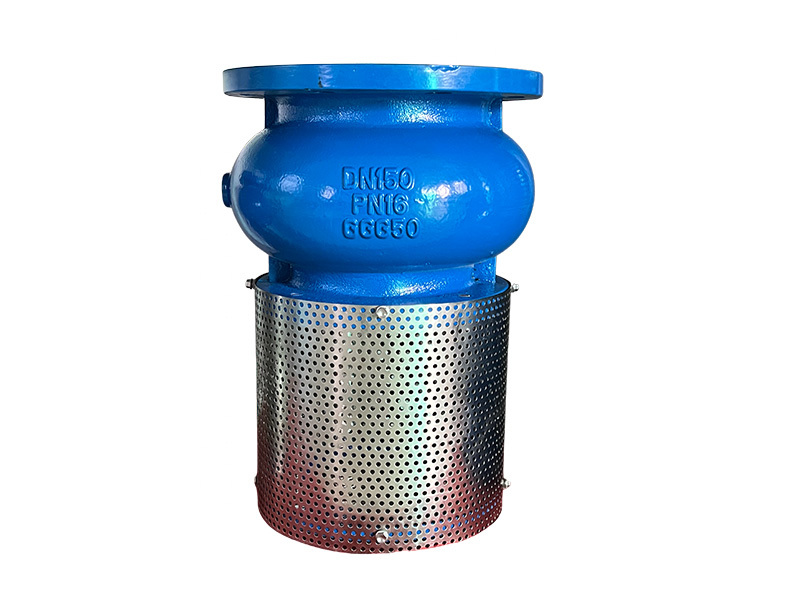
Zhengzhou Little Boy Valve Development Co., Ltd. is a joint-stock enterprise. Located in Gaoshan Town, 25 kilometers away from Zhengluo 310 National Road, it is a professional research, development, production and sales of various medium and low pressure valves. The products adopt GB,JB,ANSI,DIN,BS standard production. The products include: air valve, foot valve, (non)-rising soft seal gate valve, (non)-rising hard seal gate valve,


LITTLE BOY

quality assurance

The company has a quality control and testing center, after-sales service and technical consulting center, with strong design, development and production capabilities.

productive power

From initial product design to qualified delivery, the entire product  production  process  is  strictly  in  accordance with the  ISO9001  international  quality  assurance  system for production and after-sales service.

Customized production

Products are widely used in petrochemical, water supply and drainage, natural gas, electric power, pharmaceutical and other industries.

24-hour after service

The products are mainly exported, sold to more than 30 countries in Europe, Africa, America and Asia, and are well received by customers.

The Role of Basket Strainers in Enhancing Pipeline Filtration

The Role of Basket Strainers in Enhancing Pipeline Filtration Table of Contents Introduction to Basket Strainers What Are Basket Strainers? The Benefits of Using Basket Strainers How Basket Strainers Work Types of Basket Strainers Installation and Maintenance of Basket Strainers Applications of Basket Strainers in Industry Common Issues with Basket Strainers and Solutions Freque

Oct 02,2026

Innovations in Air Release Valve Technology for Enhanced Fire Safety

Innovations in Air Release Valve Technology for Enhanced Fire Safety Table of Contents 1. Introduction to Air Release Valves and Fire Safety 2. The Importance of Air Release Valves in Fire Suppression Systems 3. Recent Advancements in Air Release Valve Technology 4. Innovative Designs and Materials for Modern Air Release Valves 5. Applications of Air Release Valves in Fire Saf

Oct 02,2026

Understanding Flanged Foot Valves: Essential Components for Industrial Fluid Management

Flanged foot valves are specialized devices designed to prevent the backflow of fluid while allowing for the intake of liquid in suction applications. They are commonly used in situations where a pump must draw fluid from underground sources, such as wells or tanks. The flanged design allows for secure attachment to piping systems, facilitating installation and ensuring a tight seal that minimizes

Oct 01,2026

The Impact of Quality in Industrial Gate Valve Manufacturing: Ensuring Precision and Reliability

The Impact of Quality in Industrial Gate Valve Manufacturing Industrial gate valves play a crucial role in various sectors, including oil and gas, water management, and chemical processing. Given the demanding environments in which these valves operate, **the quality of their manufacturing is paramount**. This article explores the multifaceted impact of quality, highlighting its significance in pe

Sep 30,2026

Swing Check Valve: Reliable One-Way Flow Control for Safer and More Efficient Piping Systems

A swing check valve provides a straightforward mechanical solution by allowing fluid to move in the intended direction while automatically closing when flow reverses.

Sep 29,2026

Understanding Double Eccentric Butterfly Valves: Design, Benefits, and Applications

Double eccentric butterfly valves, also known as double offset butterfly valves, are essential components in various industrial applications due to their distinctive design and functionality. Unlike traditional butterfly valves, which have a single point of rotation, double eccentric butterfly valves feature two offset points of rotation. This unique design minimizes friction between the disc and

Sep 29,2026

The Critical Importance of Check Valves in Ensuring Water Pipeline Safety

The Critical Importance of Check Valves in Ensuring Water Pipeline Safety Water pipelines are the arteries of our urban infrastructure, delivering essential resources to homes, industries, and municipalities. As such, it is crucial to ensure their safety and efficiency. One of the unsung heroes in this regard is the **check valve**. This article explores the pivotal role of check valves in enhanci

Sep 28,2026

Understanding the Importance and Functionality of Automatic Air Release Valves

Automatic air release valves are essential components in numerous industrial applications, particularly in systems involving fluid transport, such as water supply networks, wastewater treatment facilities, and industrial processing plants. Their primary function is to automatically release trapped air or gas from pipelines, which can otherwise lead to inefficiencies and operational issues. One of

Sep 27,2026

Exploring the Benefits of Customized Tilting Check Valves for Industrial Applications

In the industrial realm, the role of valves is paramount, and among them, customized tilting check valves stand out for their unique design and functionality. These valves are engineered to allow fluid flow in one direction while preventing backflow, a crucial feature for maintaining system integrity and efficiency. By tailoring these valves to specific operational requirements, industries can sig

Sep 27,2026

The Critical Importance of Air Release Valves in Safeguarding Water Pipeline Integrity

The Critical Importance of Air Release Valves in Safeguarding Water Pipeline Integrity Table of Contents 1. Introduction to Air Release Valves 2. Understanding Water Pipeline Damage 3. The Mechanism of Air Release Valves 4. Types of Air Release Valves 5. Benefits of Using Air Release Valves 6. Installing Air Release Valves: Best Practices 7. Maintenance and Repair of Air Release Val

Sep 26,2026

GET FREE SIMPLES


We will contact you as soon as we see your information!